Related Topics:
Ceramic Injection Molding Process-
Ceramic ferrule injection molding process
The process comprises the following steps: sequentially drying, mixing, preforming, crushing, injection molding, thermal debinding, sintering, grinding and the like. In addition, this paper also will present the step by step of the processes in designing sprue, runner, gating system and the micro mould itself. There were three analysis methodologies involved, aim-analysis, approach and filling-analysis. Its manufacturing requirements are very high, and parameters such as dimensional accuracy, roundness, and surface roughness need to meet standards to ensure the performance and reliability of. The invention also discloses a production process of the zirconia ceramic ferrule. The ceramic ferrule manufacturing process is divided into two parts, namely blank manufacturing and.
[PDF Version]
-
Injection Molded Connector Box Manufacturing Process
Connector manufacturing process involves four critical technical stages: stamping, plating, injection molding, and assembly. Each stage requires precise quality control and advanced manufacturing technologies to ensure reliable electronic connector production. After cooling and. Engineers create detailed 3D models of the connector using CAD software such as CATIA, SolidWorks, or Creo. For a typical board-to-board connector with a 0. Assembly Automated systems insert metal contacts into. Precision connector molds are the fundamental tooling required to mass-produce high-performance electronic interconnects used in automotive, medical, and consumer electronics industries. These blueprints guide the creation of molds that can withstand high pressures and temperatures during production. You benefit from the precise machine movements.
[PDF Version]
-
Standard Manufacturing Process for Cable Trays
Every reputable cable tray manufacturer starts with high-grade steel materials that meet specific industry standards for strength, durability, and corrosion resistance. The initial processing involves cutting raw steel sheets to precise dimensions using advanced laser. Cable tray manufacturing involves creating trays that are designed to hold, support, and protect electrical cables in various environments. Cable trays are crucial for organizing cables, keeping them safe from physical damage, and ensuring their proper functioning over time. Understanding the. cable trays are equivalent. The mechanical and electrical characteristics, tests, certifications, overall quality management, recommendations mentioned in this technical guide only apply to our own cable management ranges and cannot under any circumstances be transposed to si osure, overheating or. association representing the major electrical equipment manufac-turers in the U.
[PDF Version]
-
Fiber Optic Cable Loading Process
Optical fibers require special care during installation to ensure reliable operation. Installation guidelines regarding minimum bend radius, tensile loads, twisting, squeezing, or pinching of cable must be followed.
-
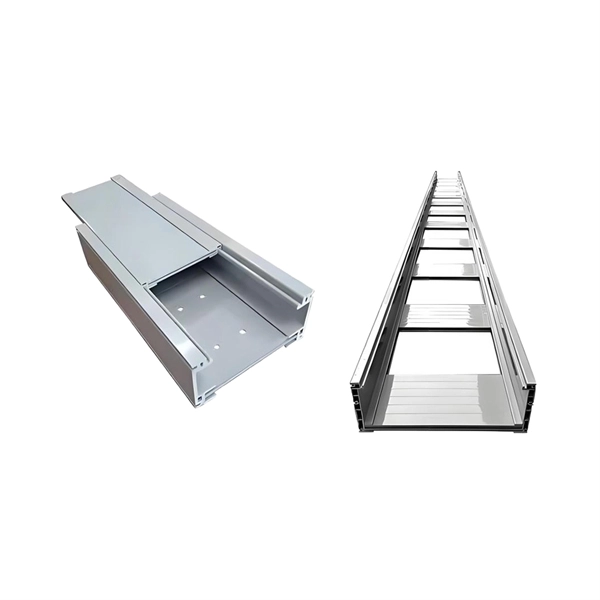
Cable tray tee processing and manufacturing process
Cable tray manufacturing relies on a coordinated production line of specialized machines: a roll forming line shapes the profile, a CNC press brake handles secondary bending, a punch press creates mounting holes and ventilation slots, and a shearing line cuts the finished tray to. Cable tray manufacturing relies on a coordinated production line of specialized machines: a roll forming line shapes the profile, a CNC press brake handles secondary bending, a punch press creates mounting holes and ventilation slots, and a shearing line cuts the finished tray to. Cable tray manufacturing involves creating trays that are designed to hold, support, and protect electrical cables in various environments. Cable trays are crucial for organizing cables, keeping them safe from physical damage, and ensuring their proper functioning over time. Together. Cable tray making machines are used to manufacture cable trays – an important component in electrical installations and industrial buildings for routing cables and wires safely.
[PDF Version]
-
ADSS Optical Cable Splicing Process
This guide provides general recommendations for the selection of methods, equipment, and tools for the stringing of ADSS (All Dielectric Self-upporting) fiber optic cables including short and Long Span ADSS cables. Since there are numerous practices which may be utilized, Prysmian has tested and determined that the practices described herein are effective and efficient. The recommended. In the process of installing the optical cable, it needs to go through the process of fusion splicing. Optical fiber consists of a core, cladding, and a protective outer coating. Each installation will be influenced by local conditions.
-
High-speed optical cable welding process
By delivering highly concentrated energy through fiber-optic cables, this technology enables ultra-precise, high-speed welding with minimal distortion. This article explores the mechanics of fiber laser welding and provides an in-depth look at its machining capabilities and. Here is a step-by-step explanation of how fiber lasers work. The process begins with high-power semiconductor laser diodes that use electricity to generate light. Once the electricity enters the diodes, an extra electron transforms into a photon.
-
The Entire Process of Optical Fiber Communication Cables
Fibre-optic communication involves transmitting a signal as light, converting electrical signals to optical signals at the transmitter end and reversing the process at the receiver end. Light acts as a carrier wave and can be modulated to carry information. Step 1: Preparing the Raw Material – Silica The first stage in making a fiber optic cable begins with the raw material: silica (silicon dioxide). The silica is refined and shaped into large. The manual is intended as a guide for technologists, middle-level management, as well as regulators, to assist in the practical installation of optical fibre-based systems. Throughout the discussions on the practical issues associated with the application of this technology, the explanations focus. An optical fiber is a single, hair-fine filament drawn from molten silica glass.
[PDF Version]
-
What are the standards for exposed ceramic ferrules
DIN 46228-4: 2020-03 defines the ferrules with insulation collars from 0. In addition to the color and size variants not defined in the standard, the Phoenix Contact portfolio also includes the uninsulated ferrules described in DIN 46228-1. Ferrules offer many advantages in mechanical and electrical terms in electrical engineering systems. When using. All Standard Ferrules are precision manufactured according to strict quality standards. Custom Ferrules are made of alumina or zirconia ceramics. Ceramic ferrules are short, cylindrical or sleeve-shaped components made from refractory ceramic material — typically high-alumina or mullite-based compositions. They are inserted into the ends of boiler tubes where those tubes meet a tube sheet or refractory wall, and in some designs, they extend. Ceramic ferrules and sleeves are often used in optical connectors, attenuators, fiber stubs, and other optoelectronics requiring low signal loss. The Specifications given below are common but not limited to. Maximum 1450 Deg Celsius to 1650 Deg Celsius.
[PDF Version]